Aluminum powertrain
Ask about built-up edge, PCD edge condition after interrupt, and whether a carbide backup tool is quoted for the 0.500 in land.
FREE sourcing support for qualified business buyers, with an eligible benefit of up to 3%. Eligibility applies to qualified business buyers and is confirmed after we review your product, quantity, destination, and sourcing requirements.
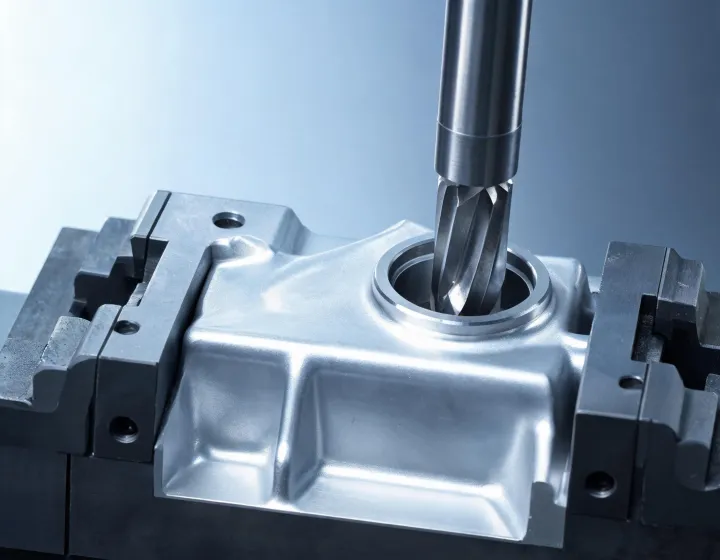
APPLICATION REQUIREMENTS
A PCD reamer manufacturer quote for a hydraulic-block shop finishing 0.500 in bores is only readable when bore material, interruption pattern, coolant, and the holder decision are written down. This page turns common US project uses into purchase questions, not into claimed factory case counts.
Send an application briefAsk about built-up edge, PCD edge condition after interrupt, and whether a carbide backup tool is quoted for the 0.500 in land.
Delamination risk and dust control belong on the RFQ. Confirm if edge inspection photos are included.
PCD may be the wrong family. Ask the bidder to justify substrate against the print before price is used.
Move to the catalog family. Cleanliness and ISO 13485 scope stay factory-side until copies arrive.
A hydraulic-block shop finishing 0.500 in sealing lands may need tighter Ra than locating bores. Split the tolerance table instead of tightening every diameter.
Prototype carbide grind and later PCD production should be two quantity lines with two inspection plans.
| Finished diameter and length | State the 0.500 in land in inches or mm and which lands are functional. |
|---|---|
| Flute / coolant | Through-coolant presence changes grind and price on interrupted hydraulic ports. |
| Shank and holder | HSK, BT, or modular coupling must match the machine list; add chucking versus floating holder. |
| Inspection | CMM, optical, or edge-microscope method plus cylindricity after ream report format. |
|---|---|
| Documents | Material cert, CoC, and any customer-specific PPAP fields. |
| Destination | Hydraulic-block plant address, Incoterm, and whether tryout pieces travel separately. |
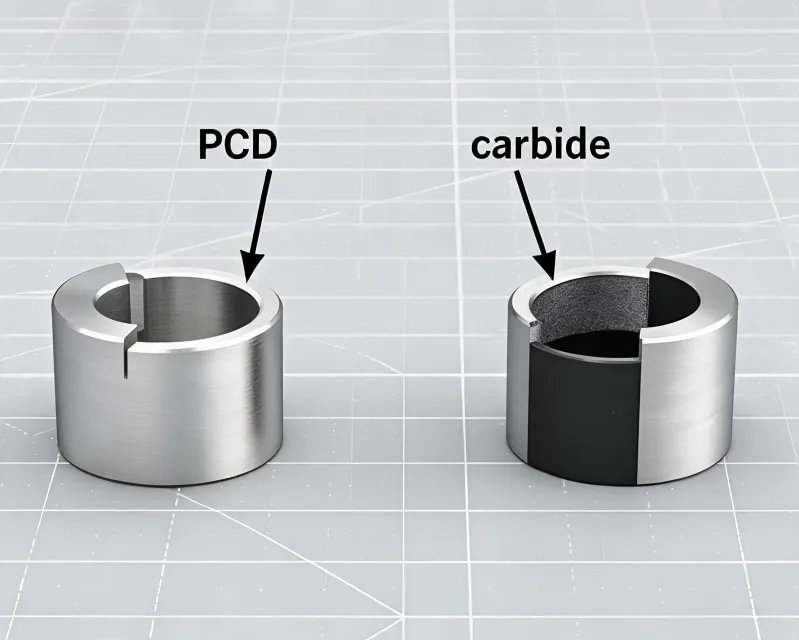
US teams often see a lower ex-works number from Asia and a shorter holder-tryout loop from a domestic grind shop. Ocean freight, duty, and IP handling change the winner. This site does not publish a 20-40% saving as its own result.
Engineering may keep ±0.005 mm on a 0.500 in sealing land. Opening non-functional diameters to ±0.1 mm can remove grind passes. Ask factories to price both stacks.
A rigid chucking reamer can hold cylindricity when the hydraulic-block fixture is already aligned. A floating holder can save a slightly off spindle, yet it can also mask a tapered grind. Write the holder and the cylindricity after ream method on the same line as price.
Coolant type, tool-changer length, and tryout window on the 0.500 in cell belong on the RFQ. A factory that never sees the machine list is guessing.
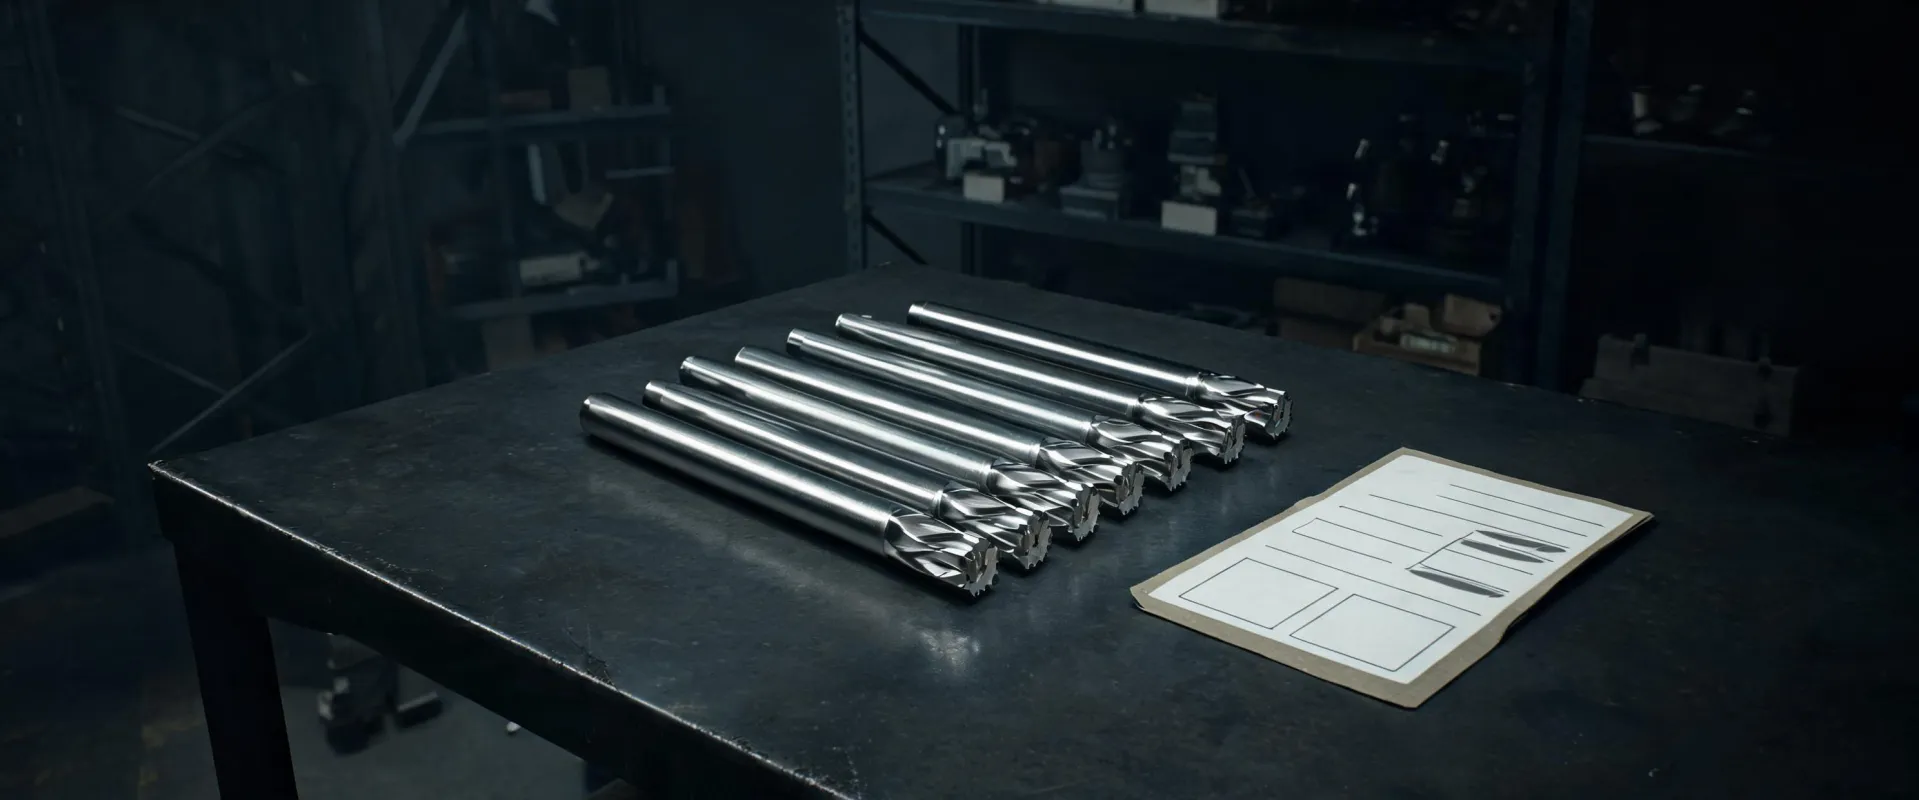
Include intended bore material, delivery stage, documents, holder type, and site constraints. We then ask factories for wholesale quotations against that same hydraulic-block packet.